Thermodynamic Loading at the Containment Boundary: Why Thermal Transients Destabilize Static Shell Seals
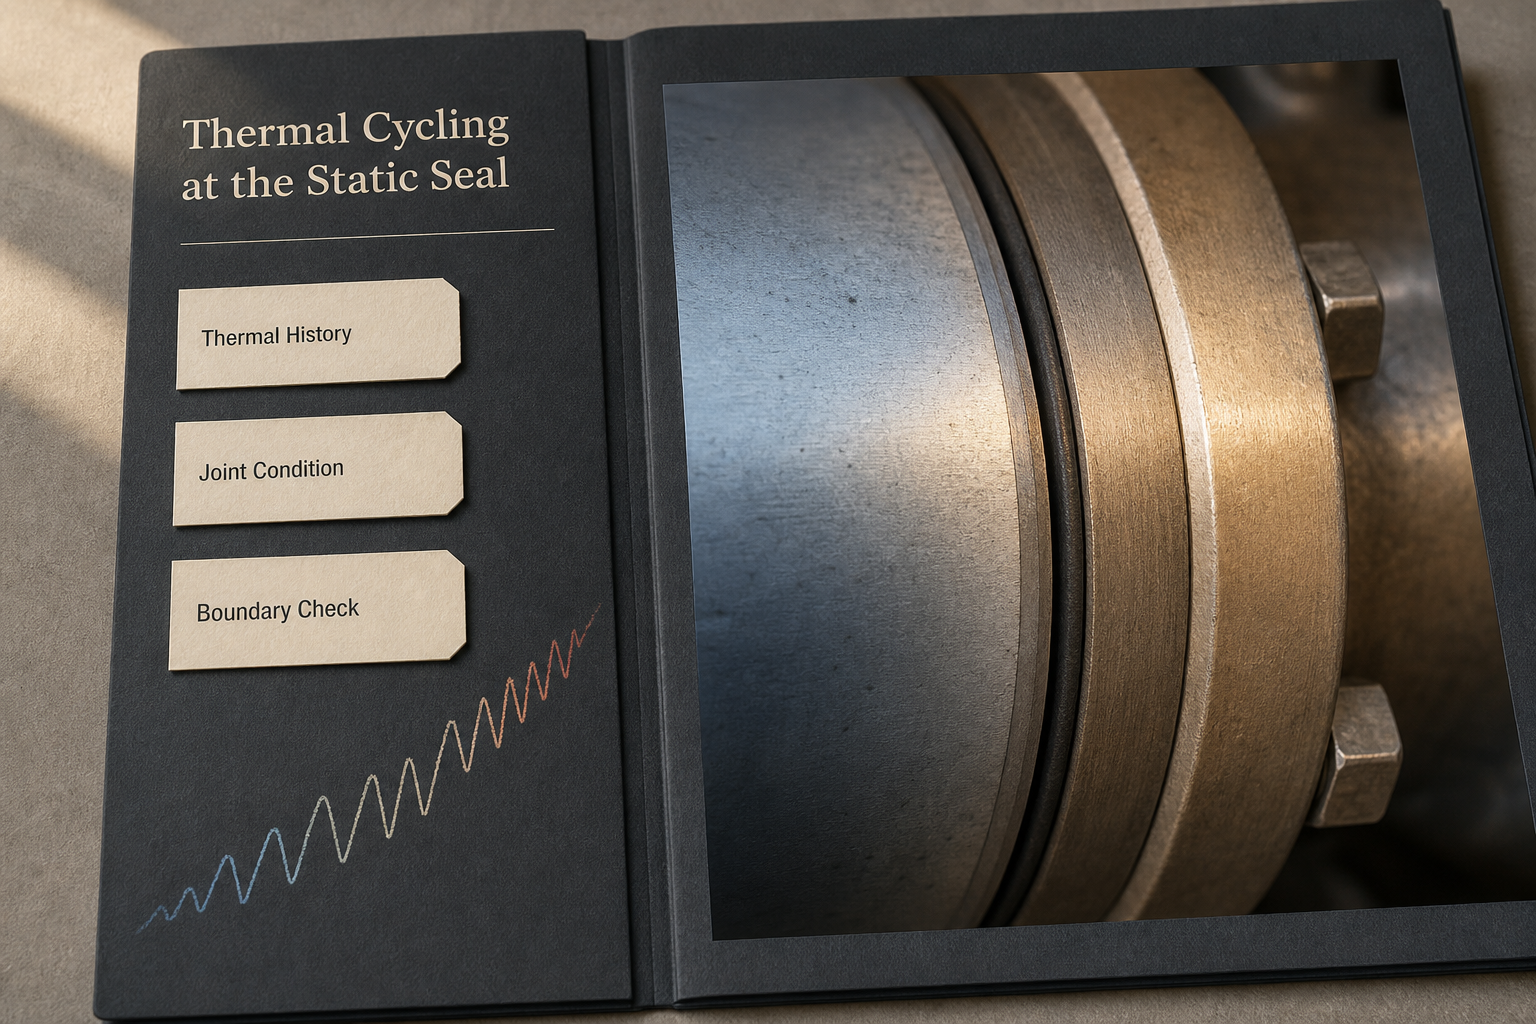
In sealless magnetic-drive centrifugal pumps, the containment shell forms the primary pressure boundary isolating hazardous, toxic, and volatile chemicals from the ambient environment. The static containment joint is simultaneously subjected to hydraulic process pressures, structural nozzle loads, and severe internal thermal transients. During batch operations, CIP/SIP steam cycles, or wide-temperature chemical swings, this static boundary undergoes repetitive thermal cycling.
Under cyclic temperature swings, containment shell static seal integrity depends on continuous preservation of compressive contact stress. However, thermal gradients across the joint induce differential thermal expansion between the metallic casing flange and thin-walled containment shell. Concurrently, alternating thermal expansion cycles accelerate bolt preload relaxation, cyclic gasket creep, and elastomer compression set.
When localized contact stress decays below the critical threshold required to seal micro-machined surface asperities, the static boundary develops microscopic leak paths. During cooling transients, geometric shrinkage mismatches induce transient micro-breathing, drawing in air or weeping volatile vapors. Establishing an engineering understanding of coupled thermal-mechanical stress evolution across the containment joint is essential for ensuring absolute containment integrity.
Heat Generation and Dissipation Kinematics: Eddy-Current Losses and Transient Temperature Fields
Magnetic Flux Shearing and Localized Eddy-Current Heating
In metallic containment shells (Hastelloy C-276, Titanium, 316L Stainless Steel), the shell resides within the narrow annular gap between the rotating outer magnet assembly and inner magnet rotor. High-speed rotation of permanent magnetic flux lines induces eddy-current electrical losses within the metallic shell wall. This energy converts directly into localized thermal power, generating substantial heat flux that elevates containment shell operating temperatures up to 150°C to 250°C.
Internal Lubrication Flush Circulation and Cooling Flow Disruption
To prevent thermal accumulation, magnetic-drive pumps utilize an internal bypass fluid stream routed from the discharge casing across the containment cavity to lubricate sleeve bearings and dissipate eddy-current heat. If internal flush passages suffer from vapor binding, particulate clogging, or flow reduction, heat removal rates drop sharply. Localized thermal spikes propagate axially into the containment shell flange land, superimposing steep thermal gradients upon the static sealing boundary.
Differential Thermal Expansion and Interfacial Shear Across Heterogeneous Flange Joints
Differential Thermal Expansion Mismatch Across Metallic and Non-Metallic Shells
The containment boundary comprises heterogeneous material components exhibiting distinct coefficients of thermal expansion (CTE, α). Forged steel pump casings (α ≈ 11.5 × 10⁻⁶/K) operate in direct contact with thin-walled Hastelloy shells (α ≈ 11.2 × 10⁻⁶/K), austenitic stainless steels (α ≈ 16.5 × 10⁻⁶/K), or non-metallic composite shells (CFRP, PEEK, Zirconia Ceramics with α ≈ 3.0 to 8.0 × 10⁻⁶/K). As operating temperatures fluctuate, these CTE differentials generate unequal radial and axial expansions.
Radial Thermal Shear and Micro-Scuffing Along the Sealing Land
Unequal thermal expansion rates between the rigid casing flange and the flexible containment shell generate cyclic radial displacement differentials (Δr = r · Δα · ΔT). This relative radial motion imposes cyclic shear stresses across the static seal contact face. Over repeated thermal cycles, interfacial micro-scrubbing shears elastomeric sealing lips, abrades composite gasket binders, and produces fretting scuff marks on precision-machined flange lands, degrading surface conformability.
Table 1 – Thermomechanical Properties and Thermal Expansion Discrepancies in Containment-Shell Materials
| Component / Substrate | Material Grade | Thermal Expansion (α, 10⁻⁶/K) | Thermal Conductivity (W/m·K) | Max Service Temp (°C) | Interfacial Thermal Response |
| Pump Casing Flange | Cast Carbon Steel / Ductile Iron | 11.0–12.0 | 45–52 | 350 | Rigid baseline structural restraint |
| Metallic Shell (High-Nickel) | Hastelloy C-276 | 11.2 | 9.8–12.5 | 400 | Moderate expansion, high eddy-current heat |
| Metallic Shell (Austenitic) | 316L Stainless Steel | 16.0–16.5 | 15.0–16.3 | 300 | High thermal expansion, severe radial shear |
| Non-Metallic Shell (Polymer) | Carbon-Fiber Reinforced PEEK | 5.0–8.0 (radial) | 1.2–2.5 | 250 | Zero eddy currents, low radial expansion |
| Ceramic Shell (Oxide) | Yttria-Stabilized Zirconia (YSZ) | 9.5–10.5 | 2.0–3.0 | 450 | Zero eddy currents, high compressive modulus |
Mechanical Fastener Dynamics: Cyclic Bolt Creep, Flange Rotation, and Preload Relaxation
High-Temperature Bolt Elongation and Elastic Preload Decay
Containment flange sealing relies on continuous compressive clamping loads generated by high-tensile alloy studs. During operating temperature increases, elevated thermal expansion of clamped metallic flanges subjects bolts to heightened tensile stress. Under sustained thermal exposure, fastener alloys undergo microscopic dislocation climb and cyclic stress relaxation. Upon subsequent cool-down, bolt elasticity fails to fully recover, resulting in residual clamping force loss of 15% to 35% after initial thermal cycling.
Flange Elastic Angular Deflection and Uneven Gasket Loading
Thermal gradients between the hot inner containment shell boundary and cooler ambient casing exterior induce uneven thermal moments, causing localized flange angular rotation. This elastic deflection unloads the outer perimeter of the gasket while concentrating compressive stress along the inner edge. Non-uniform contact stress distribution diminishes effective sealing width, allowing internal fluid pressure to penetrate micro-voids along the unloaded gasket periphery.
Table 2 – Thermomechanical Degradation Modes in Static Sealing Interfaces Under Thermal Cycling
| Sealing Mechanism | Material / Configuration | Thermomechanical Driver | Local Micro-Phenomenon | Macroscopic Symptom | Engineering Mitigation |
| Fastener Preload Relaxation | Alloy Steel Studs (B7/B8M) | Thermal creep and joint yield | Elastic tensile strain loss | Flange joint weeping during cool-down | Disc spring washers & hot re-torquing |
| Elastomer Compression Set | Fluoroelastomer (FKM) O-Rings | Polymer cross-link degradation | Irreversible flat-spot molding | Cold startup weeping, loss of prime | Peroxide-cured FFKM or resilient U-seals |
| Interfacial Micro-Shear | Modified PTFE Gaskets | Differential radial expansion | Surface micro-tearing & creep flow | Gasket thinning, bolt torque loss | Fully confined gland pockets |
| Radial Joint Distortions | Thin-walled Hastelloy Shells | Non-uniform cooling gradients | Ovality, flange waviness | Asymmetric gasket stress distribution | Precision pilot spigot alignment fits |
Material Morphology Degradation: Compression Set, Polymer Creep, and Micro-Breathing Dynamics
Elastomeric Cross-Link Network Degradation and Compression Set (Cs)
Elastomeric O-rings (FKM, EPDM, FFKM) provide static sealing through stored elastic recovery energy. When exposed to continuous thermal cycling, elevated temperatures induce oxidative aging, polymer chain scission, and secondary cross-linking within the compressed matrix. As elastic recovery degrades, compression set (Cs) rises toward 50% to 80%. Upon cooling to ambient conditions, the elastomer cannot recover its initial cross-sectional height, completely losing contact stress against the gland ceiling.
Thermal Micro-Breathing and Fugitive Vapor Emissions
During operational shutdown, the containment joint cools faster than internal fluid volumes, creating transient differential contraction. If gasket contact stress drops below critical sealing thresholds during this transition, micro-voids open along the sealing interface—a phenomenon known as thermal micro-breathing. Sub-atmospheric internal vacuum surges or residual hydraulic pressures draw process vapors across the interface, leading to intermittent fugitive emissions that vanish when normal operating temperatures re-expand the joint.
Table 3 – Chemical and Thermal Performance Matrix for Magnetic-Drive Pump Containment Seals
| Seal Material / Geometry | Temp Capability (°C) | Chemical Compatibility | Compression Set (Cs, 150°C) | Resilience to Radial Shear | Recommended Application Boundary |
| Peroxide-Cured EPDM | -40 to +140 | Polar solvents, steam, dilute acids | Moderate (25%–35%) | High tensile elongation | Hot water, aqueous chemicals, polar fluids |
| Specialty FKM (High-Fluorine) | -15 to +200 | Hydrocarbons, fuels, aggressive acids | Moderate (30%–45%) | Moderate abrasion resistance | Petrochemical, hot solvents, mineral acids |
| Perfluoroelastomer (FFKM) | -20 to +260 | Universal chemical resistance | Low (15%–25%) | Excellent chemical integrity | Severe toxic chemicals, wide thermal swings |
| Spring-Energized Modified PTFE | -70 to +280 | Universal chemical inertness | Zero (metallic spring return) | Superior radial slip endurance | Cryogenic to ultra-high temperature loops |
Yokey Engineering Controls: Resilient Spring-Energized Architectures, Micro-Tolerance Glands, and FEA Thermal Modeling
Resilient Spring-Energized Polymer Seal Configurations
To eliminate reliance on vulnerable elastomeric memory during extreme thermal cycling, Yokey engineers high-performance spring-energized polymer sealing solutions for magnetic-drive containment boundaries. Utilizing precision-machined modified PTFE or filled fluoropolymer jackets energized by corrosion-resistant Elgiloy or Hastelloy cantilever V-springs, these seals provide mechanical live-loading. The internal metallic spring continuously compensates for thermal shrinkage, flange differential expansion, and bolt relaxation across wide thermal cycles.
Gland Geometry Optimization and Micro-Tolerance Interface Control
Yokey evaluates customer containment flange geometries—including flat face, spigot pilots, and confined groove profiles—recommending optimized groove dimensions, anti-extrusion clearances, and micro-surface finishing (Ra ≤ 0.4 μm) based on application CAD drawings and pressure ratings. Proper confinement limits polymer cold flow under high containment pressures, controls thermal expansion during temperature transitions, and protects the primary sealing boundary against fluid shear. Precision CNC turning maintains strict geometric concentricity and smooth surface micro-finishing, eliminating microscopic leak paths.
Non-Linear Thermomechanical Coupled Finite Element Analysis (FEA)
Yokey applies advanced coupled thermomechanical FEA modeling to simulate temperature distributions, thermal displacement vectors, and contact stress evolution across the complete casing-shell-flange assembly. Non-linear simulations model bolt preload relaxation, transient thermal gradients during startup and cooldown, and contact pressure retention across gasket interfaces, ensuring sealing contact stress remains comfortably above critical seating thresholds across the entire thermal lifecycle.
Application-Specific Engineering Review: The Yokey 4-Step Containment Thermal Evaluation Workflow (CTA)
When chemical processing plants experience intermittent cold-start weeping, containment joint pressure decay, or premature seal embrittlement, Yokey provides a structured technical review via the Yokey 4-Step Containment-Shell Thermal Interface Evaluation:
1. Thermal-Cycle Parameter Profiling: Plant engineers submit operating envelopes (ΔT swing, cycle frequencies, fluid media, and ramp rates) directly to eric.h@nbyokey.com for boundary review.
2. Coupled FEA Stress Modeling: Simulation of transient thermal gradients, differential radial displacement (Δr), and bolt clamp load decay across the customer flange assembly.
3. Resilient Sealing Profile Matching: Selection of live-loaded spring-energized PTFE profiles, metal-reinforced gaskets, or specialty FFKM formulations suited to the thermal envelope.
4. Machining and Assembly Control Specification: Defining precision gland tolerances, surface micro-roughness standards, and disc spring bolt torque protocols ensuring long-term joint reliability.
FMEA Risk Matrix: Failure Mode and Effects Analysis for Containment-Shell Static Sealing
Table 4 – Failure Mode and Effects Analysis (FMEA) for Magnetic-Drive Pump Containment Shell Static Seals
| Failure Mode | Direct Failure Cause | Local Interface Effect | System-Level Effect | Detection Method | Engineering Control Action |
| Radial Shear Abrasion | CTE mismatch (Δα) between shell and flange | Micro-fretting and lip scuffing along land | Intermittent vapor leakage on cooldown | Helium sniffing and optical profilometry | Customized gland geometries & PTFE seals |
| Fastener Preload Decay | Thermal bolt creep under elevated cycling | Gasket clamping stress drops below seating | Fluid weeping during operational cooldown | Residual torque audit & ultrasonic stretch | Belleville disc springs & hot re-torque |
| Elastomer Thermal Set | Polymer cross-link breakdown at peak temp | Permanent flattening (Cs > 60%) | Total loss of seal recovery when cooled | Hardness testing and micrometer C-S check | Deploy Yokey spring-energized U-seals |
| Gasket Extrusion Flow | Thermal softening under internal pressure | Polymer cold-flows into clearance gap | Sealing land thinning, abrupt blowout | Visual teardown and gap inspection | Precision PEEK anti-extrusion back-up |
| Thermal Micro-Breathing | Differential shrinkage during shutdown | Micro-gaps open under negative pressure | Atmospheric ingress or vapor escape | Bubble testing and VOC sniff detectors | Resilient live-loaded spring energizers |
| Eddy-Current Overheat | Insufficient cooling flow bypass circulation | Severe local thermal degradation of seal | Rapid seal charring, fluid leakage | Thermographic camera & casing sensor | Optimize internal bypass flush channels |
Physical Validation Path: 5-Stage Protocol for Containment-Shell Thermal Integrity
To establish rigorous engineering verification for static seals operating under severe thermal cycling, Yokey recommends a structured 5-stage validation protocol:
Stage 1 – Dimensional Metrology and Flange Flatness Profiling: Verify casing flange flatness, spigot pilot concentricity, and groove surface roughness (Ra ≤ 0.4 μm) against engineering drawings using 3D coordinate measuring machines (CMM) and optical non-contact profilometry to eliminate geometric stress risers.
Stage 2 – Thermal Shock and Cyclic Pressure Simulation: Assemble containment joints into dedicated pressure test fixtures. Cycle fluid temperatures across defined limits (-20°C to +200°C) at ramp rates exceeding 10°C/min for 500 thermal cycles under continuous 2.5 MPa hydraulic holding pressure.
Stage 3 – Sub-Atmospheric and High-Pressure Vacuum Leak Profiling: Subject cycled containment assemblies to helium mass spectrometry sniffing under 10⁻⁵ mbar·L/s sensitivity, verifying absolute zero-leakage containment under both positive hydraulic heads and full internal vacuum conditions.
Stage 4 – High-Temperature Accelerated Compression Set Aging: Subject elastomeric and polymer test coupons to continuous thermal soaking at maximum operating temperature (200°C) for 1,000 hours. Measure residual tensile strength, elongation retention, and compression set (Cs) recovery percentage.
Stage 5 – Full-Scale Pump Dynamic Thermal Run Validation: Install validated containment seal assemblies into full-scale magnetic-drive process pumps. Execute 500-hour continuous run testing incorporating cyclic fluid batch transfers, monitoring casing thermography, eddy-current heat dissipation, and containment boundary integrity.
Comprehensive Engineering Synthesis: Ensuring Absolute Containment in Hazardous Process Pumping
In magnetic-drive sealless pumps, the static containment shell seal serves as the ultimate barrier against hazardous fluid releases. Maintaining this boundary across prolonged operational campaigns requires recognizing that thermal transients impose severe, coupled thermomechanical stresses that cannot be resolved through generic gasket selection or passive torque tightening.
Differential thermal expansion, localized eddy-current heating, cyclic fastener preload relaxation, and elastomer compression set represent an interrelated chain of physical mechanisms leading directly to joint micro-breathing and interfacial leakage. Engineering durable containment requires matching flange geometry, selecting resilient materials capable of mechanical live-loading, and optimizing thermal dissipation pathways.
By deploying live-loaded spring-energized PTFE seals, utilizing precision-confined gland architectures, executing non-linear coupled thermomechanical FEA modeling, and enforcing multi-stage physical validation, chemical processing operations can achieve absolute, leak-free containment reliability across the most demanding high-temperature and cyclic fluid duties.
Frequently Asked Questions (FAQ)
Q: Why does a containment-shell static seal frequently weep during operational cooling rather than at peak operating temperature?
A: During peak temperatures, elevated thermal expansion increases thermal expansion forces, temporarily boosting gasket clamping stress. During cooldown, rapid thermal contraction combined with irreversible bolt preload relaxation and elastomer compression set causes clamping stress to drop sharply, opening transient micro-gaps before mechanical stabilization occurs.
Q: How does eddy-current heating in metallic containment shells affect static seal life?
A: High-frequency magnetic shearing generates localized internal heat within metallic shells (Hastelloy, Titanium), creating steep axial temperature gradients up to 200°C near the flange land. This localized heat accelerates elastomer cross-link scission and thermal gasket creep, requiring specialized cooling circulation to protect the joint.
Q: What is the main operational advantage of spring-energized PTFE seals over standard elastomeric O-rings in thermal cycling duties?
A: Spring-energized PTFE seals rely on an internal metallic cantilever or coil spring to maintain continuous mechanical live-loading. Unlike elastomers, which suffer permanent compression set and chemical hardening at elevated temperatures, the metallic spring continuously expands and contracts, compensating for thermal shrinkage during cycling.
Q: How does differential thermal expansion (CTE mismatch) induce static seal degradation?
A: When a casing flange and containment shell expand at different rates (such as carbon steel vs. stainless steel), relative radial displacement creates interfacial shear scrubbing. This cyclic sliding motion abrades gasket contact surfaces, wears elastomer sealing lips, and generates micro-leak paths across the flange land.
Q: What role do Belleville disc spring washers play in maintaining containment flange preload?
A: Belleville spring washers provide substantial elastic compliance within the fastener stack. When bolts undergo thermal elongation or flange gaskets experience minor creep, the disc springs expand to maintain continuous clamping tension, mitigating up to 80% of cyclic bolt preload decay.
Q: Why are non-metallic containment shells (such as CFRP or Ceramic) less prone to localized thermal seal degradation?
A: Non-metallic materials do not conduct electricity, completely eliminating eddy-current electrical losses and associated localized heat generation. Operating temperatures at the sealing boundary remain close to bulk fluid temperatures, substantially reducing thermal stress gradients across the joint.
Q: How can plant maintenance teams distinguish between chemical degradation and thermal fatigue failure on containment O-rings?
A: Chemical degradation typically manifests as uniform volumetric swelling, surface blistering, softening, or gummy dissolution across the entire exposed seal profile. Thermal fatigue induces localized permanent flat-spotting (compression set), radial micro-cracking, hardening, and circumferential micro-fretting scuff marks along the sealing contact band.
Q: When should plant reliability engineers submit pump operating dossiers for a Yokey containment thermal evaluation?
A: Plant engineers should submit operating parameters and CAD drawings to eric.h@nbyokey.com whenever magnetic-drive pumps experience cold-start vapor weeping, recurring bolt torque decay after thermal batch cycles, premature gasket hardening within 12 months, or when upgrading process duties to aggressive chemicals operating above 150°C.
Post time: Oct-13-2026